
Shop Now
-
Welding Consumables
-
MIG Welding Wires
- Mild Steel MIG Wires
- Stainless Steel MIG Wires
- Duplex & Super Duplex MIG Wires
- Low Alloy MIG Welding Wires
- Flux Cored MIG Wires
- Flux Cored Seamless MIG Wires
- Flux Cored Self Shielded MIG Wires
- Flux Cored Stainless Steel Wires
- Flux Cored Duplex MIG Wires
- Aluminium MIG Wires
- Metal Cored MIG Wire
- Metal Cored Seamless MIG Wires
- Bronze MIG Wires
- TIG Welding Rods
- Welding Electrodes
- Gouging Carbons
- Hardfacing Wires
- Sub Arc Wires
- Sub Arc Flux
- Brazing Rods
- Brazing Fluxes
- Soldering Products
-
MIG Welding Wires
- Welding Torches and Torch Spares
-
Welding Machines
- Machine Bundles
- MIG Welding Machines
- TIG Welding Machines
- STICK Welders
- Multi-Process Welders
- Battery Welders
- Laser Welders
- Laser Cleaners
- Wire Feeders
- Sub Arc Welding Machines
- Stud Welding Machines
- Engine Driven Welding Machines
- Weld Cleaning Machines
- Welding Automation Machines
- Heating Equipment
- Tungsten Grinders
- Tungsten Feeders
- Plasma & Cutting Machines
-
Welding Machine Spare Parts
- Welding Trolleys
- Alfra Spare Parts
- Betaweld Spare Parts
- Bug-O Spare Parts
- Cougartron Spare Parts
- Excision Spare Parts
- Fronius Spare Parts
- Geiger Spare Parts
- Hypertherm Spare Parts
- Kemppi Spare Parts
- Koike Spare Parts
- Lincoln Electric Spare Parts
- Miller Spare Parts
- Neutrix Spare Parts
- Rex Spare Parts
- Taylor Spare Parts
- Unimig Spare Parts
- Von Arx Spare Parts
- Weldmax Spare Parts
- Welding Fume Extraction Equipment
- Gas Welding Equipment
- Welding Abrasives
-
Welding Safety Gear
- Welding Helmets
-
Welding Helmet Spares
- Speedglas Welding Helmet Spares
- 3M Spares
- Betaweld Welding Helmet Spares
- Cigweld Welding Helmet Spares
- Flip Front Helmet Spares
- Jackson Welding Helmet Spares
- Lincoln Welding Helmet Spares
- Miller Welding Helmet Spares
- RPB Welding Helmet Spares
- Servore Welding Helmet Spares
- Unimig Welding Helmet Spares
- Weldclass Welding Helmet Spares
- Miscellaneous Helmet Lens
- Welding Gloves
- Protective Workwear
- Welding Blankets
- Welding Screens and Curtains
- Ear Protection
- Eye Protection
- Face Shields
- Hand Protection
- Head Protection
- Welding Respiratory Gear
- Sun Protection
- Hydration Products
- Fire Blankets
- Prestart Books
- Welding Safety Signages
- Safety Tags
- Hazard Tapes
-
Welding Accessories
- Air Tools
- Power Tools
- Welding Aids
- Welding Tables
- Welding Cables
- Welding Leads
- Electrical Power Supplies
- Welding Clamps
- Clamp Accessories
- Earth Clamps
- Welding Cleaning Equipment
- Welding Chemicals
- Arcair Gouging
- Lifting Accessories
- Hammers
- Manual Arc Accessories
- Weld Measuring
- Weld Testing Products
- Wire Brushes
- Pipe Welding Equipment
-
Cutting & Drilling
- Bandsaws
- Bandsaw Blades
- Bandsaw Accessories
- Cold Saws
- Core Drills
- Cutting Blades
- Diamond Blades
- Drill Bits
- Holesaws
- Magnetic Base Drills
- Metal Working Lubricants
- Pipe Bevelling Machines
- Pipe Cutting Equipment
- Tee Pulling Kits
- Pipe Threading Machines
- Plasma Table Water Additives
- Hydraulic Punching Machines
- Welding Merchandise
- Gift Cards
- Welding Clearances
-
Welding Equipment Hire
- Hire Equipment
- Hire Heating Equipment
- Hire Degausing Equipment
- Hire Welding Automation
- Hire a Welding Positioner
- Hire a Turning Roll
- Hire a Diesel Welder
- Hire a Wirefeeder
- Hire a Multi-Process Welder
- Hire Welding Accessories
- Hire a MIG Welder
- Hire a TIG Welder
- Hire a Stick Welder
- Hire a Plasma Cutter
- Hire a Weld Cleaner
- Hire a Stud Welder
Can You Weld Cast Iron? Your Complete Guide
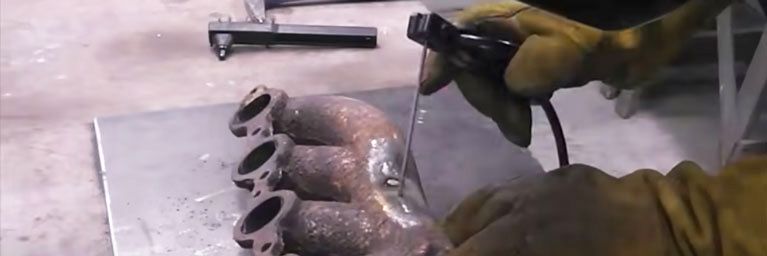
Welding cast iron is quite a challenge, but if you rigorously follow the recommended guidelines, you may be able to repair cast iron parts with little or no cracking.
Discover why welding cast iron is so difficult, how to weld it, and which welding rods are best to use for cast iron.
The Biggest Challenge with Cast Iron Welding
Cast irons are iron-carbon alloys with 2-4% carbon content, about 10x the carbon amount in most steels. There are many cast iron types, but our guide focuses on grey cast iron because it’s the most commonly used. Keep in mind that it’s impossible to weld white cast iron, while all other types are weldable.
While cast irons are hard, strong and machinable, they have poor ductility, making them incredibly difficult to weld. Welding any metal causes expansion and contraction as the material heats and cools. However, since cast iron has low ductility, especially in the fusion zone, the residual stresses from expansion and contraction can cause weld cracking.
When you weld mild steel, a ductile material, as the weld and the fusion zone expand and contract, the surrounding material can “flex.” However, cast iron doesn’t deform before breaking - it just breaks. So, when the weld cools and starts pulling the surrounding cast iron mass, it can easily crack.
To make things worse, the welding process can create locally-enriched carbon zones, and on rapid cooling, the heat affected zone (HAZ) can become extremely hard and brittle. That’s why cast iron is susceptible to HAZ cracking and generally considered challenging to weld.
How to Weld Cast Iron
It’s possible to weld cast iron using oxy-acetylene and stick arc welding (SMAW). You can also join cast iron parts by brazing, but the bond cannot match the welding strength.
Welders commonly use the stick welding process for cast iron. Its high-temperature arc allows fast travel speeds, and you can use lower preheat temperatures. In addition, stick welding can be used with a DCEN (electrode negative) polarity, which can help you reduce HAZ. Make sure to use a quality arc welder like the Kemppi Minarc Evo 140VRD, or the more powerful version, Kemppi Minarc Evo 180VRD. Your welder should have a stable and predictable arc output to avoid inconsistencies. Since cast iron is a sensitive material, you don’t want to use poorly optimised machines.
Prepare the Part for Welding
Removing all surface oil, paint, grease, and casting skin is crucial. In addition, remove the residual graphite from the surface using mineral spirits. Pay particular care to the weld area.
If the joint requires grooves, use a V groove with a 60-90° included angle. It’s helpful to create grooves around cracks and joints to ensure maximum penetration and avoid surface-only welds.
Controlling the Heat
Preheating the cast iron is the key step in avoiding weld cracking. You should preheat the entire casting slowly and evenly, if possible. As the part is heated, it will expand. As a result, it can easily crack if there is a thermal gradient over its volume. However, if the heat is applied evenly, there won’t be any localised spots resisting expansion that can crack.
Preheating will also allow the casting to cool slowly, decrease the thermal gradient between the HAZ and the rest of the part, and reduce the residual stresses. Typical preheating temperatures for cast irons are 260-650 degrees Celsius (500-1200°F). Never preheat above 760°C (1400°F).
Stagger the welds during the welding process whenever possible. Use the least amount of amperage and avoid making welds longer than ten times your electrode’s diameter.
Allow the casting to cool slowly after welding to prevent residual stresses and cracking. You can put it in sand or cover it with specialised welding blankets to prevent rapid heat loss.
Welding Rods for Cast Iron
Nickel alloy welding rods (AWS A5.1 Eni-CL) are the most commonly used electrodes for welding cast iron, and for a good reason. Nickel electrodes create a ductile weld metal that remains soft and machinable. The welds will have reduced stresses and improved resistance to cracking.
Need Additional Help?
Welding cast iron is tricky, even for highly experienced welders. If you need further assistance in equipment and filler metal selection, reach out to the experts at Alphaweld. Give us a call on (08) 9456 8000 or get in touch and our team will gladly assist you.